
Engineering teams often turn to global suppliers for machined, cast, or formed metal parts to gain capacity, capability, or cost advantages. The gains can vanish, though, when specifications do not survive translation across time zones and processes. Tolerance drift after plating, heat-treat warpage, or ambiguous datums can turn a routine RFQ into weeks of rework. This article offers a practical, specification-first approach to sourcing that keeps dimensions, finish, and function intact from CAD to delivery. It focuses on drawings that travel, material and process choices that match the design intent, how to manage secondary operations, the inspection plans that actually prevent scrap, and logistics details that protect parts in transit.
Drawings That Survive Translation: GD&T, Datums, and Default Tolerances
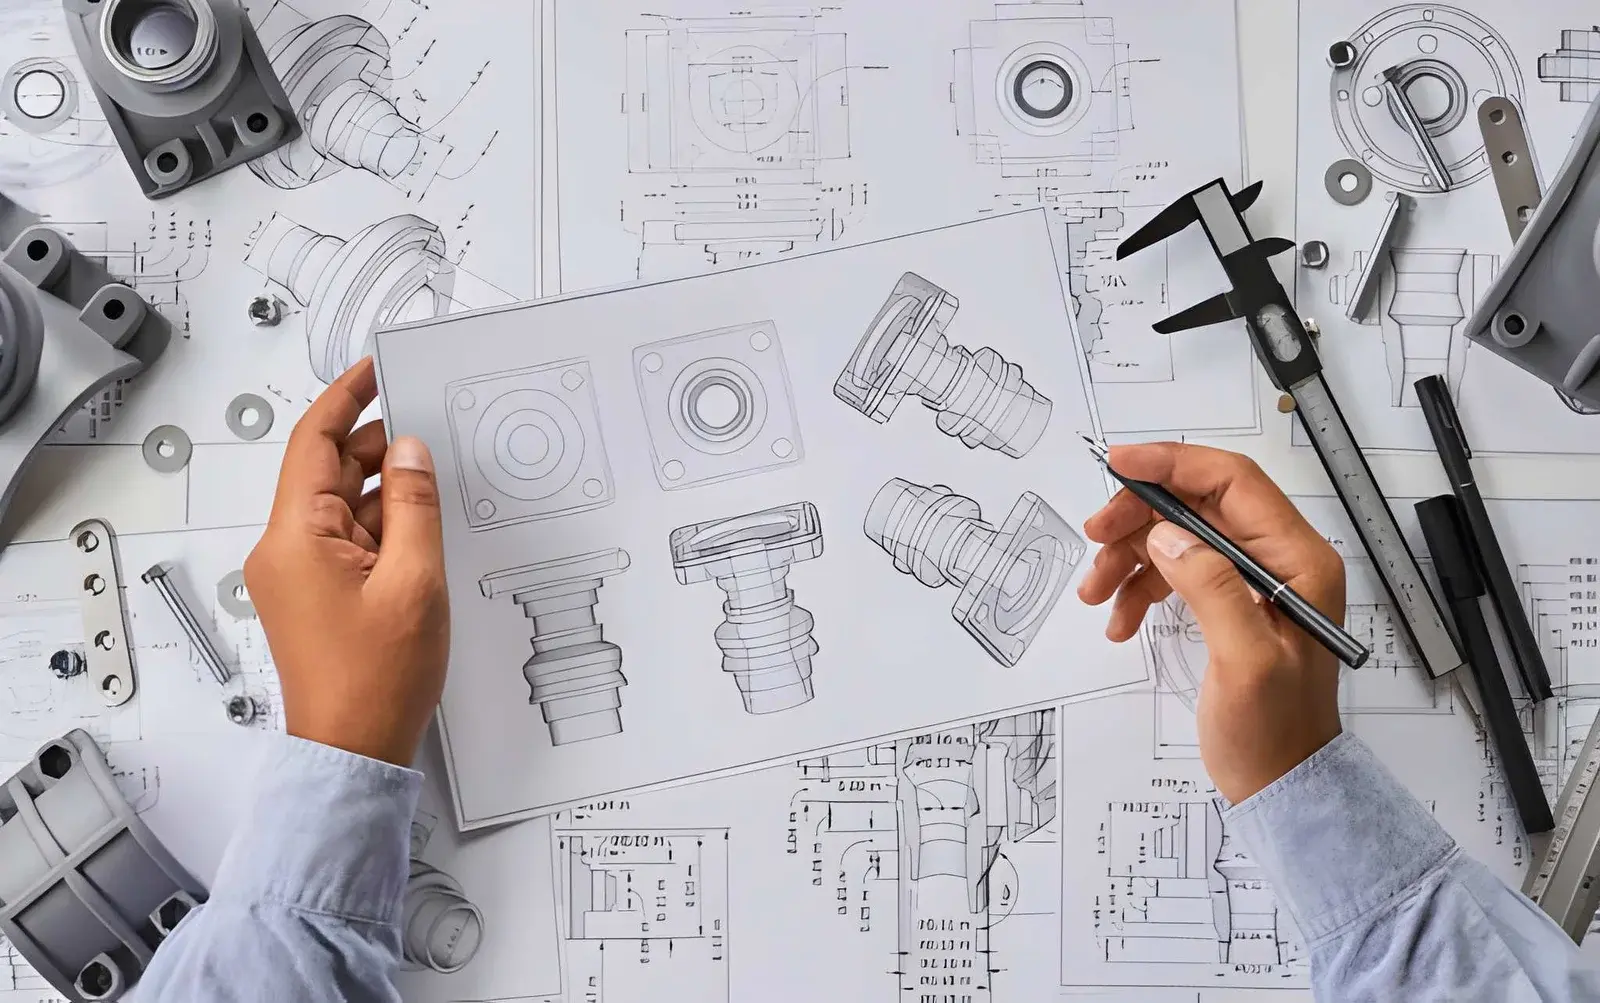
Start with a drawing that needs no interpreter. Define a clear datum scheme rooted in function, use ASME Y14.5 geometric tolerancing where relationships matter, and remove guesswork about units, default tolerances, and finish. A simple note like “Unless otherwise specified: ISO 2768-mK” or “ASME Y14.5, decimals ±0.005 in” sets a baseline that prevents shops from applying their own defaults. Call out thread forms and classes (for example, 1/4-20 UNC-2B or M6 x 1), specify surface roughness (such as Ra 63 µin), and distinguish reference dimensions from critical-to-function features. When dimensions and datums are explicit, you reduce the chance that a vendor reorients the part on a different face and shifts the entire tolerance stack.
Provide the same facts digitally and on paper. Include native CAD and a STEP file tied to the released revision, and list any model-to-drawing deviations so machinists do not chase geometry that is not actually required. If you rely on profile or position tolerances, state the gauge or measurement method intended (CMM to a datum reference frame versus functional go/no-go gauges). Suppliers that specialize in precision metal parts, such as BMF Industrial, will usually ask for this detail because it defines fixturing and inspection from day one.
Material and Process Pairings That Control Cost and Capability
Alloy and process drive both capability and price. Consider machinability, strength, and corrosion resistance together with the manufacturing route. For CNC parts, 6061-T6 aluminum machines quickly and anodizes well for enclosures, while 7075-T6 brings higher strength at the cost of reduced corrosion resistance. Free-machining 303 stainless enhances throughput compared with 304, but 304 wins for welded or corrosive environments. For ferrous parts, 1018 or 1045 are economical for turning, whereas 4140 prehardens balances wear resistance with machinability. These choices shape cycle time, tool life, and achievable tolerances before you set a single dimension.
Match process to geometry. A380 aluminum die casting favors thin walls and high volumes, but dimensional stability depends on tool design and post-cast machining stock. Investment casting handles complex stainless shapes but may require generous draft and post-cast straightening. For flat parts with consistent grain needs, stamping and laser cutting offer speed, yet grain direction and burr control must be specified to avoid fatigue issues. Each path presents a trade-off: forging or die casting can reduce unit cost at volume but adds tooling investment and lead time; fully machined parts avoid tooling but raise material removal and cycle time.
Plan for Secondary Operations: Coatings, Heat Treat, and Dimensional Growth
Many sourcing problems trace to what happens after machining or casting. Coatings add thickness and can choke fits if you do not plan for them. Zinc plating and electroless nickel deposit on every exposed surface, reducing hole size and increasing shaft diameter. Anodizing builds and penetrates; Type II decorative anodizing changes dimensions less than hardcoat, but both matter on H7-like fits. State whether tolerances apply before or after finish, and call out masking where threads, ground bores, or sealing faces must remain untouched. A practical approach is to oversize holes pre-plate or ream after plating depending on cost and capability at the supplier.
Heat treatment changes hardness and geometry. Quench-and-temper can introduce bow and twist on long parts, and case hardening can shrink thin features. Two proven sequences are rough machine, heat treat, then finish grind critical surfaces; or, for stable alloys, finish machine and specify controlled temper to limit movement. When plating high-strength steels, add hydrogen embrittlement relief baking notes. Without these clarifications, a lot that measures fine after machining may fail functionally after the final process, creating rework on the wrong side of the ocean.
Inspection That Catches Problems Early: FAI, CMM, and Certifications
Agree on how compliance will be proven before production starts. A First Article Inspection (FAI) tied to your ballooned drawing confirms the datum scheme, measurement methods, and results on a real part. List critical-to-function dimensions that must be 100 percent inspected, and allow sampling on non-critical features with an AQL or similar plan. If you specify position or profile tolerances, require a CMM report referenced to the defined datums rather than a hand tool check from an arbitrary setup. Ask for material test reports (for example, EN 10204 3.1 certificates), hardness results for heat-treated parts, and coating thickness readings when fit matters. Catching a misaligned dowel hole in FAI with a go/no-go pin gauge costs hours; catching it after 1,000 pieces are plated costs weeks.
Packaging and Logistics That Protect Metal Parts in Transit
The spec’s last mile is the box. Sea freight exposes parts to humidity for weeks, so pair VCI (vapor corrosion inhibitor) bags, desiccants, and corrosion-inhibiting oils where compatible. Separate precision faces with paper or foam interleaves to prevent fretting. Block and brace heavy items in crates to avoid edge dents. Label cartons with part number, revision, lot, and quantity to maintain traceability. Define Incoterms that fit your risk tolerance: EXW and FOB shift control earlier in the chain; DAP centralizes responsibility but affects cost. Poor packaging can undo perfect machining, so treat protective measures as part of the drawing, not an afterthought in the warehouse.
Global metal parts sourcing works best when specifications lead, and every downstream decision reflects them. A drawing that travels, a material-process pairing that suits function, secondary operations that are measured rather than assumed, inspection that targets risk, and packaging built for the route each eliminate one source of surprise.” When teams handle these details up front, they turn far-flung suppliers into stable extensions of their own shop floor. Treat every RFQ as the start of a control plan, and the parts arriving on your dock will look, fit, and perform the way the CAD model promised.
Also Read
